Engineering Reliable
Vacuum Solutions
for Modern Industries.
High performance vacuum pumps, vacuum systems and accessories engineered for maximum efficiency, reliability and long service life — across chemical, pharma, food, power and process industries.
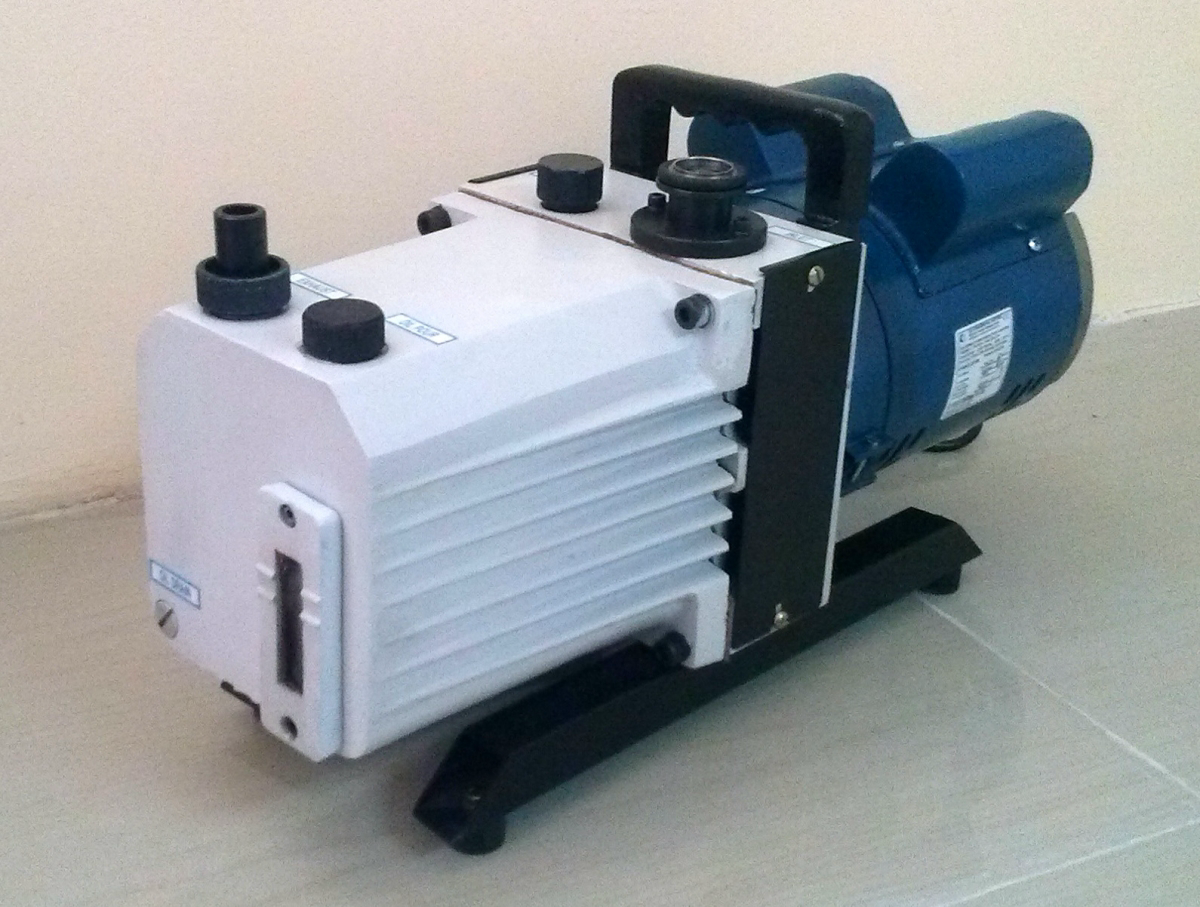
Trusted across critical process industries.
Our vacuum pumps and systems run continuously in some of the most demanding industrial environments — engineered for the duty, not just the data sheet.
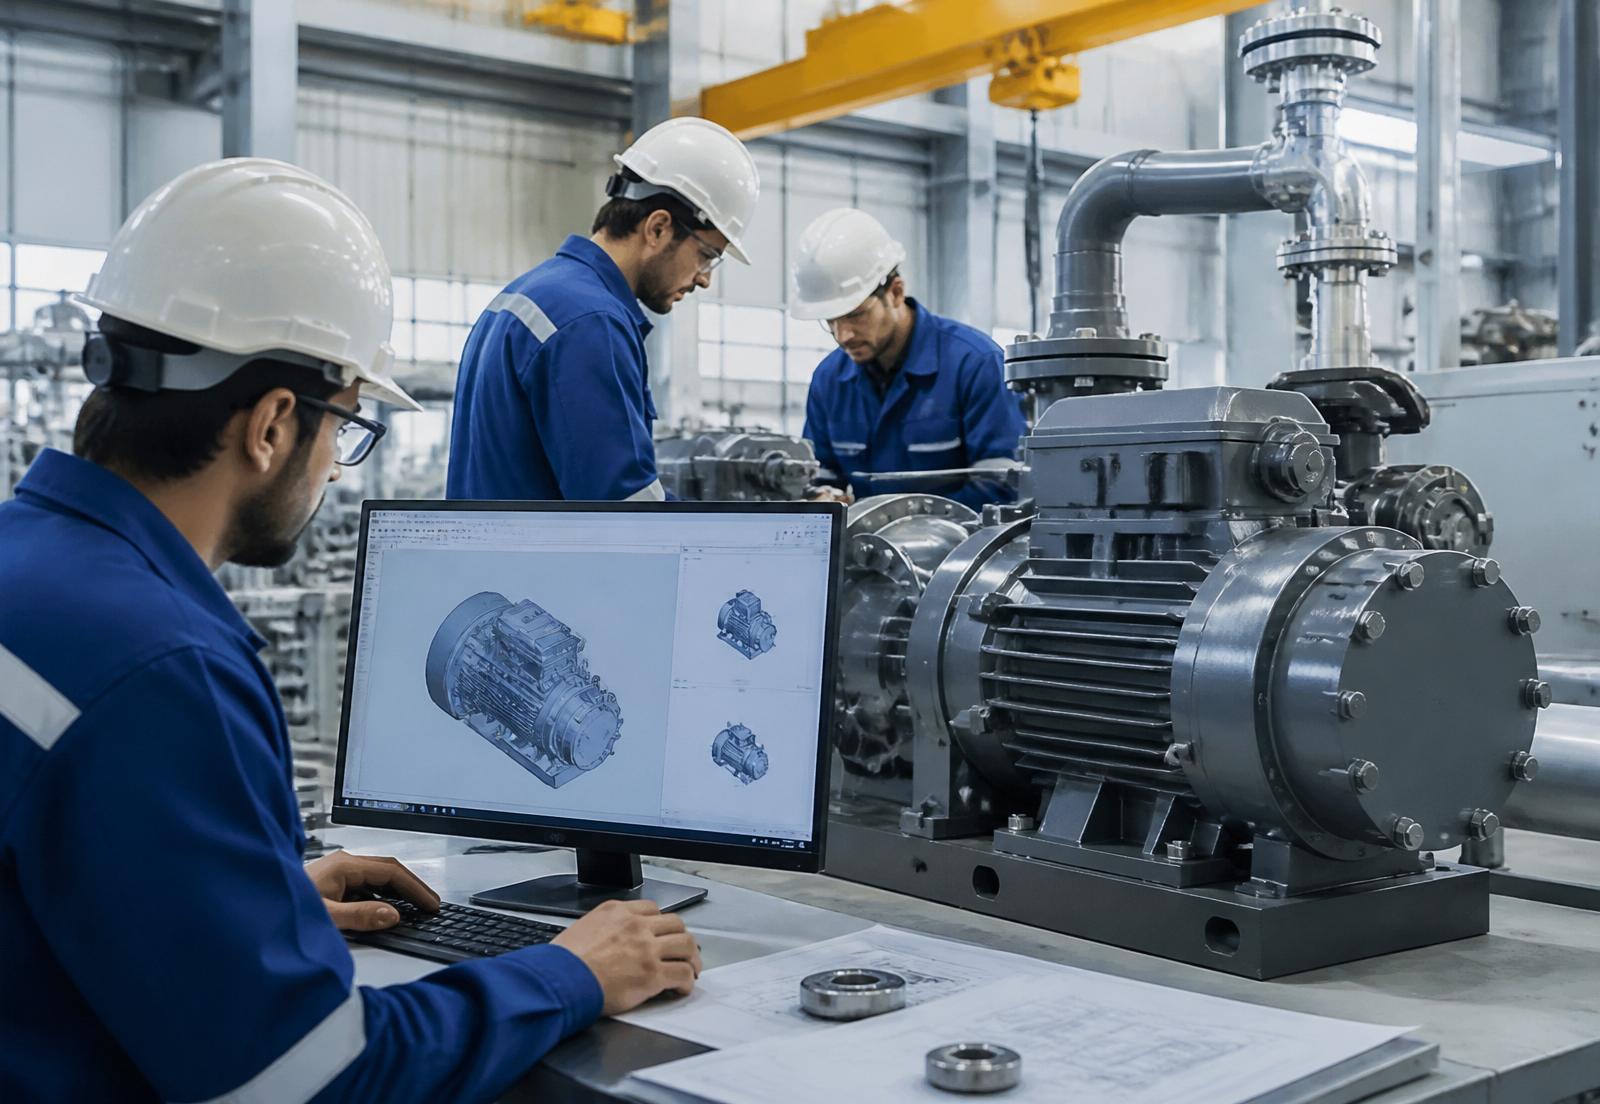
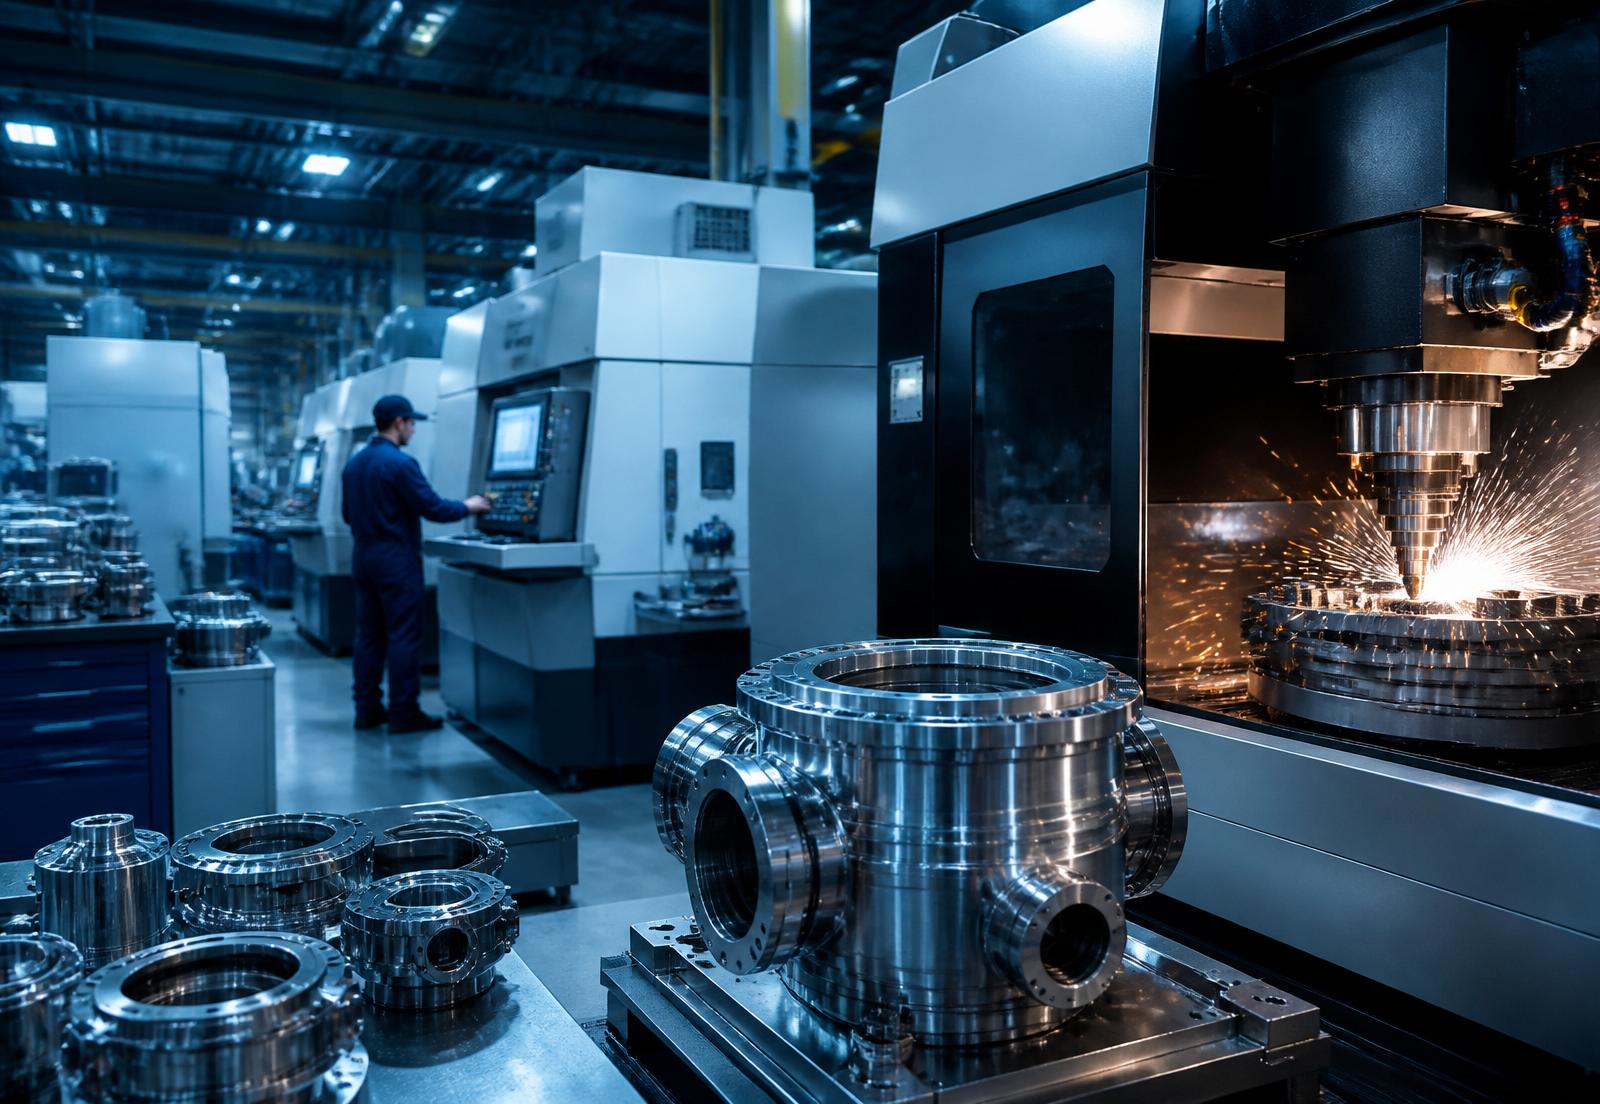
A techno-driven engineering company built on precision.
Headquartered in Bangalore, India, we design and manufacture high-quality vacuum pumps, vacuum systems and accessories for process industries worldwide. Every product is engineered for performance, reliability and a long service life.
- Modern manufacturing facility
- International quality standards
- Experienced engineering team
- Custom engineered solutions
- Energy efficient products
- Environment friendly approach
Vacuum pumps and engineered systems.
From compact monoblock pumps to 25,000 m³/hr engineered booster systems — every product is built in-house and performance-tested before dispatch.
RotaryPortable Air-Cooled Rotary High Vacuum Pump
Portable / direct-drive air-cooled, double-stage rotary high-vacuum pumps from 50 LPM to 2,000 LPM.
- Capacity
- 50 – 2,000 LPM (3 – 120 m³/hr)
- Vacuum
- Up to 5 × 10⁻³ mbar
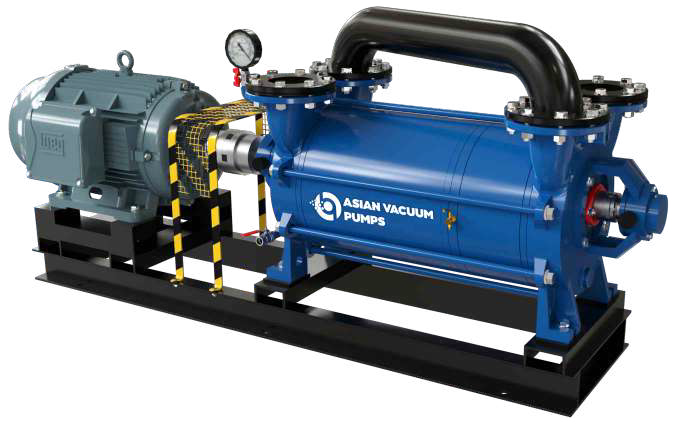 Liquid Ring
Double Stage Liquid Ring Vacuum Pump
High-efficiency two-stage liquid ring pump engineered for deep vacuum and continuous duty.
- Capacity
- 90 – 1,350 m³/hr (open suction)
- Vacuum
- 720 mm of Hg (close suction)
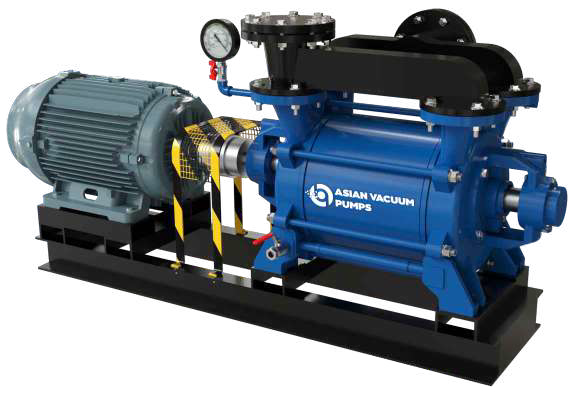 Liquid Ring
Single Stage Liquid Ring Vacuum Pump
Multi-purpose single-stage liquid ring pump — also usable as a compressor with minor modifications.
- Capacity
- 49 – 2,700 m³/hr (open suction)
- Vacuum
- 710 mm of Hg (close suction)
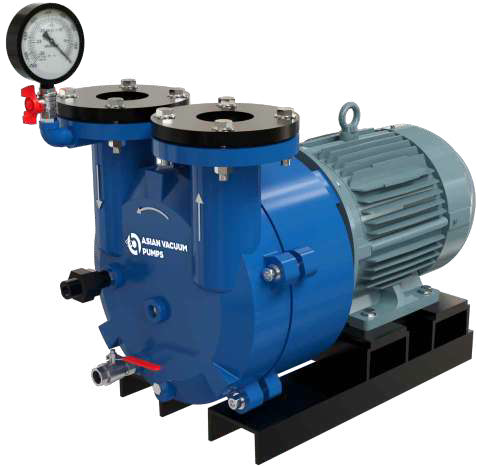 Liquid Ring
Monoblock Vacuum Pump
Compact monoblock construction with direct motor coupling for small footprint installations.
- Capacity
- 14 – 330 m³/hr (open suction)
- Vacuum
- 710 mm of Hg (close suction)
Liquid RingMBP Series Liquid Ring Vacuum Pump
Engineered series with twin-port suction and improved efficiency for chemical and pharma duty.
- Capacity
- 150 – 7,000 m³/hr
- Vacuum
- Up to 40 mbar abs
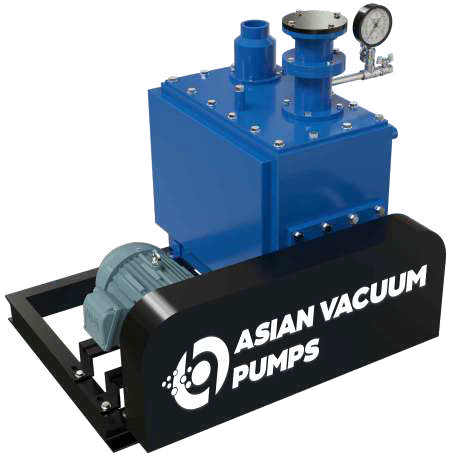 Rotary
Oil Seal Vacuum Pump
Oil-immersed rotary vane pump delivering high vacuum from 1.8 CFM to 708 CFM — single- and two-stage.
- Capacity
- 1.8 CFM to 708 CFM (50 – 20,000 LPM)
- Vacuum
- 0.05 mm Hg (single stage) · 0.005 mm Hg (two stage)
Engineering depth that delivers in the field.
Years of process-pump engineering, combined with in-house manufacturing and a hands-on service team.
Modern CNC-equipped facility producing pumps to global tolerances.
Experienced design team using CFD and 3D CAD for every solution.
Bespoke vacuum systems engineered to your exact process.
Optimised hydraulics that lower kW per m³/hr of vacuum delivered.
Designed and tested to ISO, ASME and ATEX where applicable.
In-house manufacturing keeps lead times short and prices fair.
24+ technical experts on call for installation and field service.
Robust mechanical design proven in 3800+ installed systems.
Heavy-duty bearings, premium seals and serviceable internals.
Free vacuum-selection consulting from concept to commissioning.
From raw material to running plant — every step under one roof.
Our integrated facility lets us control every stage of manufacturing, from CAD design to factory acceptance testing — delivering consistent quality and short lead times.
- STEP 01Design
3D CAD modelling, CFD analysis and detail engineering.
- STEP 02Machining
CNC turning, milling and grinding to micro-tolerances.
- STEP 03Assembly
Skilled assembly cells with calibrated torque and alignment.
- STEP 04Testing
Performance, vacuum, leak and run-in tests on every unit.
- STEP 05Quality Control
Multi-stage inspection — incoming, in-process, final.
- STEP 06Packaging
Export-grade crating with anti-corrosion protection.
- STEP 07Dispatch
Pan-India and global logistics with documentation.
Where vacuum makes the process possible.
A guide to the most common applications where Asian Vacuum systems are specified by EPCs, OEMs and end users.
Compare technologies at a glance.
A quick reference to help shortlist the right vacuum technology for your duty. Need a recommendation? Talk to our engineers.
| Parameter | Single Stage LRVP | Double Stage LRVP | Oil Seal Rotary | Mechanical Booster | LR Vacuum System |
|---|---|---|---|---|---|
| Vacuum Level | 130 mbar | 33 mbar | 10⁻³ mbar | 10⁻² mbar | 33 mbar |
| Capacity (m³/hr) | 25 – 9,000 | 100 – 11,000 | 1 – 300 | 500 – 25,000 | Custom |
| Maintenance | Low | Low | Medium | Medium | Low |
| Water Required | Yes | Yes | No | No | Yes (recirculated) |
| Best For | Wet duty | Process vapours | Clean dry | Low pressure | Turnkey |
| Efficiency | ★★★★ | ★★★★★ | ★★★ | ★★★★★ | ★★★★★ |
Specified by engineers. Trusted by operators.
"Asian Vacuum's engineered booster system replaced our legacy ejectors and cut steam consumption dramatically. Commissioning was clean and the team was responsive throughout."
"We rely on their two-stage LRVPs for our distillation columns. Build quality is excellent and after-sales support has been quick and competent every single time."
"Sized our process vacuum correctly the first time. The skid arrived export-packed and was running within the week — exactly what we needed."
Frequently asked questions.
Common engineering and commercial questions answered by our application team.
Let's engineer the right vacuum solution for your process.
Share your duty conditions and our application engineers will recommend the optimum pump, capacity and configuration — usually within 24 hours.