Engineered vacuum solutions for every process.
From compact monoblock units to 25,000 m³/hr booster systems — built in-house, performance-tested, and ready for the field.
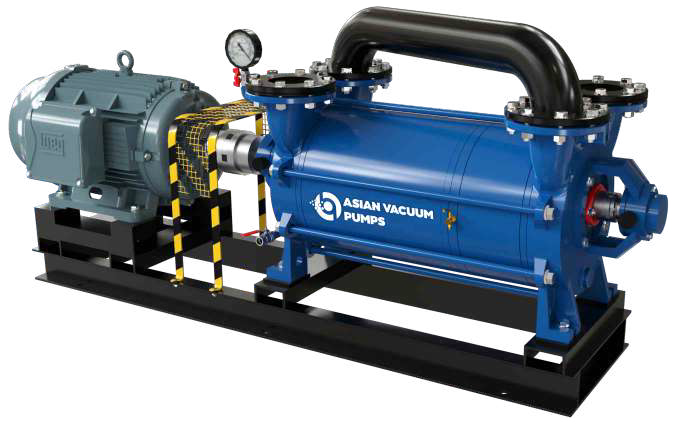 Liquid Ring
Double Stage Liquid Ring Vacuum Pump
High-efficiency two-stage liquid ring pump engineered for deep vacuum and continuous duty.
- Capacity
- 90 – 1,350 m³/hr (open suction)
- Vacuum
- 720 mm of Hg (close suction)
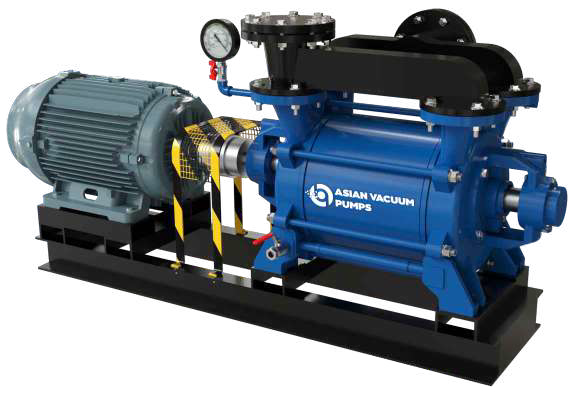 Liquid Ring
Single Stage Liquid Ring Vacuum Pump
Multi-purpose single-stage liquid ring pump — also usable as a compressor with minor modifications.
- Capacity
- 49 – 2,700 m³/hr (open suction)
- Vacuum
- 710 mm of Hg (close suction)
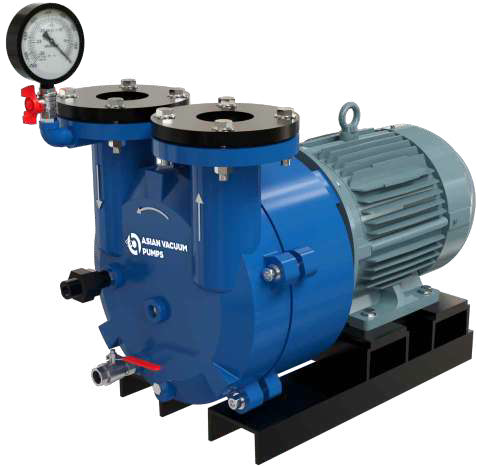 Liquid Ring
Monoblock Vacuum Pump
Compact monoblock construction with direct motor coupling for small footprint installations.
- Capacity
- 14 – 330 m³/hr (open suction)
- Vacuum
- 710 mm of Hg (close suction)
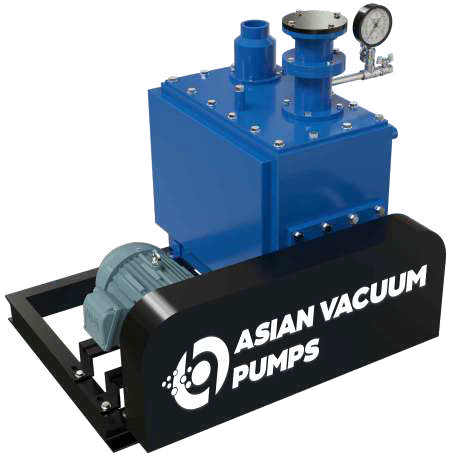
Liquid RingMBP Series Liquid Ring Vacuum Pump
Engineered series with twin-port suction and improved efficiency for chemical and pharma duty.
- Capacity
- 150 – 7,000 m³/hr
- Vacuum
- Up to 40 mbar abs
 Rotary
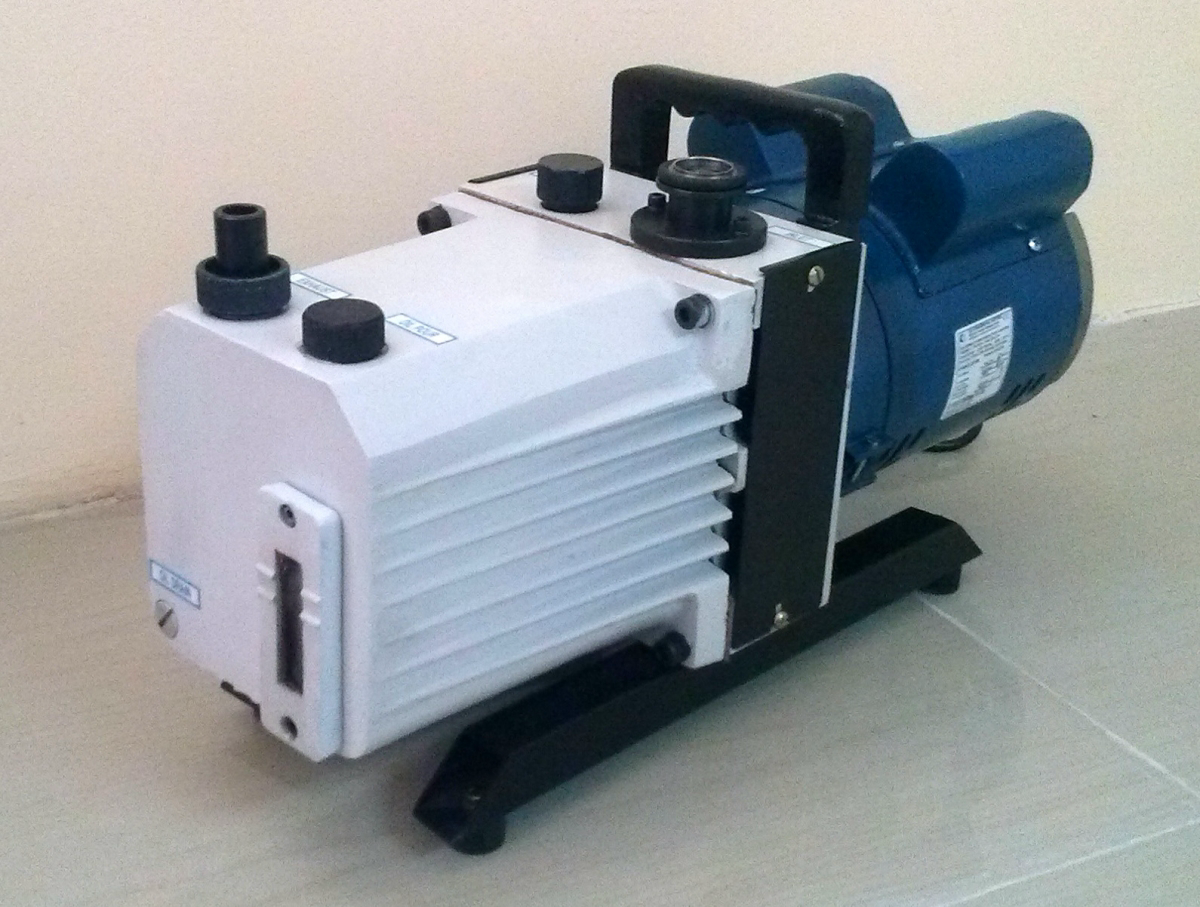
Oil Seal Vacuum Pump
Oil-immersed rotary vane pump delivering high vacuum from 1.8 CFM to 708 CFM — single- and two-stage.
- Capacity
- 1.8 CFM to 708 CFM (50 – 20,000 LPM)
- Vacuum
- 0.05 mm Hg (single stage) · 0.005 mm Hg (two stage)
 Rotary
Portable Air-Cooled Rotary High Vacuum Pump
Portable / direct-drive air-cooled, double-stage rotary high-vacuum pumps from 50 LPM to 2,000 LPM.
- Capacity
- 50 – 2,000 LPM (3 – 120 m³/hr)
- Vacuum
- Up to 5 × 10⁻³ mbar
 Systems
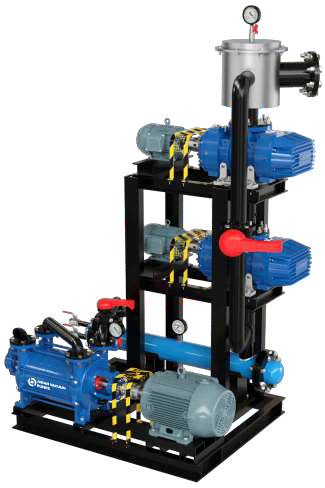
Mechanical Vacuum Booster
Roots-type mechanical booster delivering 660 LPM to 200,000 LPM suction capacity for petro-chemical duty.
- Capacity
- 660 LPM to 200,000 LPM
- Vacuum
- 0.001 Torr (max)
 Systems
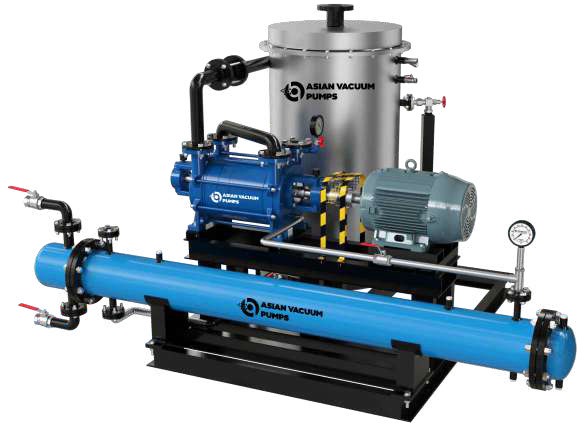
Liquid Ring Vacuum System
Complete engineered skid with pump, separator, heat exchanger, valves and instrumentation.
- Capacity
- 50 – 1,800 m³/hr (closed-loop)
- Vacuum
- From 1000 mbar to 33 mbar abs
 Systems
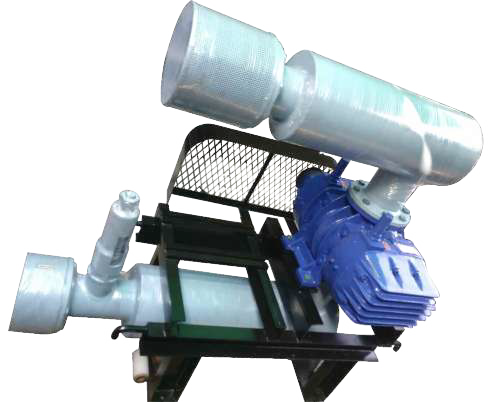
Gas Charging Board
Skid-mounted gas charging board for evacuation and refrigerant / SF₆ charging operations.
- Capacity
- Custom
- Vacuum
- 10⁻³ mbar
 Accessories
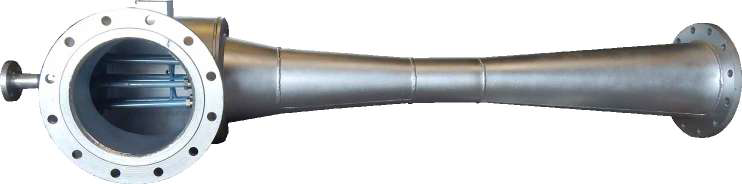
Steam Jet Ejector Vacuum System
Motive-steam driven ejector — no moving parts, ideal for hostile vapours and high temperatures.
- Capacity
- Custom — process driven
- Vacuum
- Down to 0.01 mbar (multi-stage)
 Rotary
Single Stage Rotary Vane Pump
Compact single-stage oil-sealed rotary pump for medium-vacuum duty.
- Capacity
- 50 – 20,000 LPM (1.8 – 708 CFM)
- Vacuum
- 0.05 mm Hg
 Rotary
Two-Stage Rotary Vane Pump
Two-stage oil-sealed pump for high ultimate vacuum down to 0.005 mm Hg.
- Capacity
- 50 – 20,000 LPM (1.8 – 708 CFM)
- Vacuum
- 0.005 mm Hg
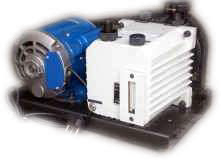 Rotary
Belt-Drive Rotary Vacuum Pump
Belt-driven air-cooled double-stage rotary vacuum pumps from 150 – 1,000 LPM.
- Capacity
- 150 – 1,000 LPM
- Vacuum
- Up to 5 × 10⁻³ mbar
Let's engineer the right vacuum solution for your process.
Share your duty conditions and our application engineers will recommend the optimum pump, capacity and configuration — usually within 24 hours.